Connecting rod
- Connecting rod inspection
- Connecting rod alignment
- Connecting rod straightening
- Big-end resizing
- Small-end bush replacement
- Small-end bush boring
- Connecting rod honing
- Connecting rod reconditioning
Engine reconditioning & precision machining facility
Connecting Rod
Restore rod bores, alignment and fastener condition. We check, measure and recondition connecting rods so each rod is straight, correctly sized and ready for the rebuilt assembly.
What this covers
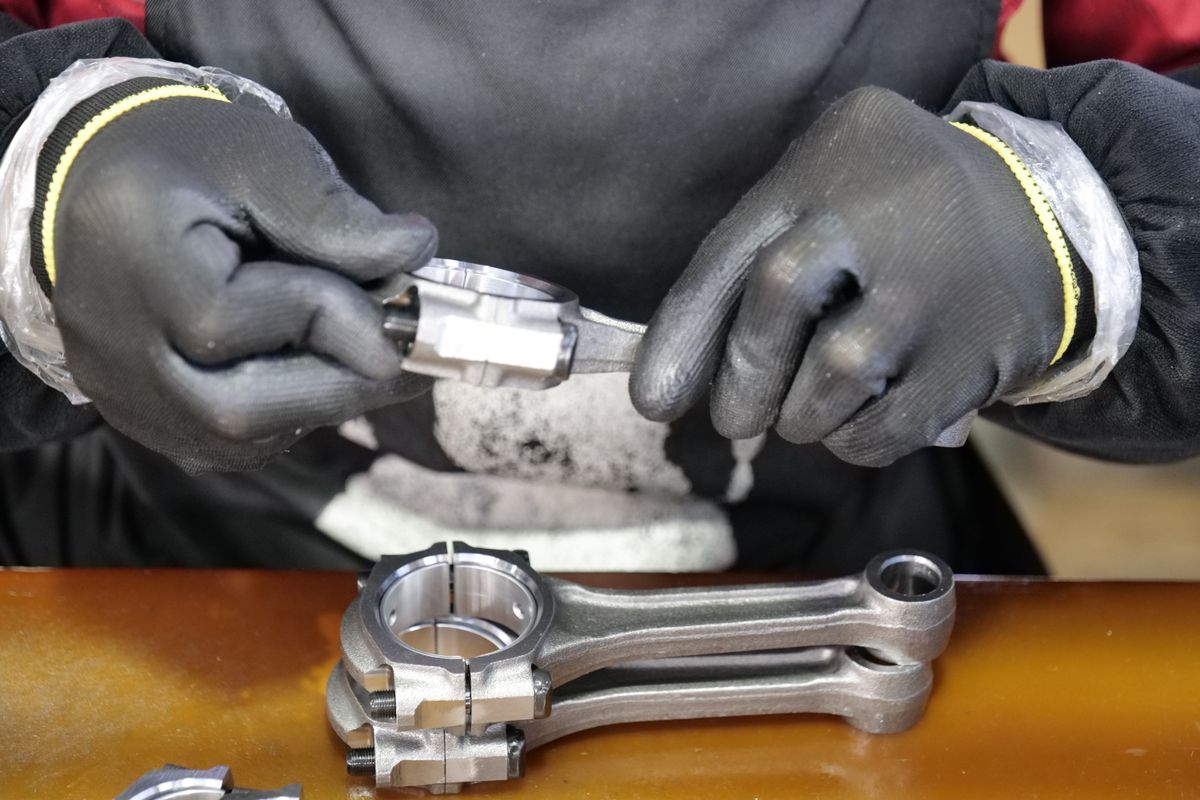
Overview
Connecting rods transfer the full force of combustion to the crank. A twisted or bent rod, or an out-of-round big-end bore, puts the whole reciprocating assembly out of true.
Each rod is checked for straightness and twist, its big-end and small-end bores are measured, and bores are reconditioned to size where required so the rod is square in the engine.
Reconditioned to measurement
Reconditioned to measurement. Not guesswork.
Decisions on connecting rod reconditioning are made from recorded measurements against specification — never from how a part “looks”.
Symptoms
These are the problems and symptoms that typically point to the component needing reconditioning work.
Sub-services
Each item is listed so you can see the full scope of this service. Machining jobs run through PRT's inspect, measure, machine and verify route; specialist processes that are arranged externally are called out in the notes.
Inspection
5 checks and measurements inform the decision to machine — nothing is cut until the component has been assessed.
Measurement & quality
A rod that is bent, twisted or out-of-round transfers stress to the crank and piston. Alignment and bore geometry are checked before assembly.
Verified after machining
PRT process
Rods are identified, cleaned and inspected, including their fasteners.
Straightness and twist are checked across the rod.
Big-end and small-end bores are measured for size and roundness.
Bores are resized where needed so bearings seat correctly.
Final geometry is verified and rods are kept with their matched caps.
Machinery & stations
Each operation is carried out at the appropriate station with the correct tooling. The stations involved in this service are:
Gallery
Authentic PRT photography of real jobs will appear here as it is captured and approved.
Connecting Rod Reconditioning work in progress at the PRT facility.
Real photography of the operation will appear here when PRT approves imagery.
Before-and-after records of PRT jobs are published as real projects.
Related services
Restore worn journals to size and true running geometry. Crankshaft grinding returns main and crankpin journals to specification for use with matching undersize bearings.
View serviceCut and finish cylinders to exact size with the correct surface finish. Boring removes the wear and taper; honing produces the plateau finish new rings need to seat.
View serviceA controlled, clean, torque-accurate build. We assemble reconditioned engines from measured components — so the finished unit leaves the shop built to specification and ready to run.
View serviceFAQ
Straight answers to the questions we expect about this service.
No — each rod is measured first. Resizing is only done where the big-end bore is outside its specification.
Fastener condition is assessed during inspection. Fasteners that are doubtful or not reusable by specification are flagged for replacement before assembly.
A rod that is bent or twisted loads the piston sideways in the bore and the journal unevenly, which shortens the life of rings, bearings and the crank itself.
Get a Quote
Tell us the engine or component, its condition and what the rebuild needs to achieve. We will confirm the scope from an actual assessment.