Skip to content

Cylinder Block

Cylinder Block Reconditioning

Strip, inspect, measure and machine the engine's foundation. We recondition cylinder blocks for rebuilds — cleaning, crack detection, boring and honing, deck surfacing and, where needed, line boring of the main bearing housings.

What this covers

  • Complete strip-down and cleaning of water jackets and oil galleries
  • Cylinder boring and honing to required size
  • Deck surfacing to restore head-sealing flatness
  • Line boring of main bearing bores when alignment is lost
  • Thread and dowel repair where required
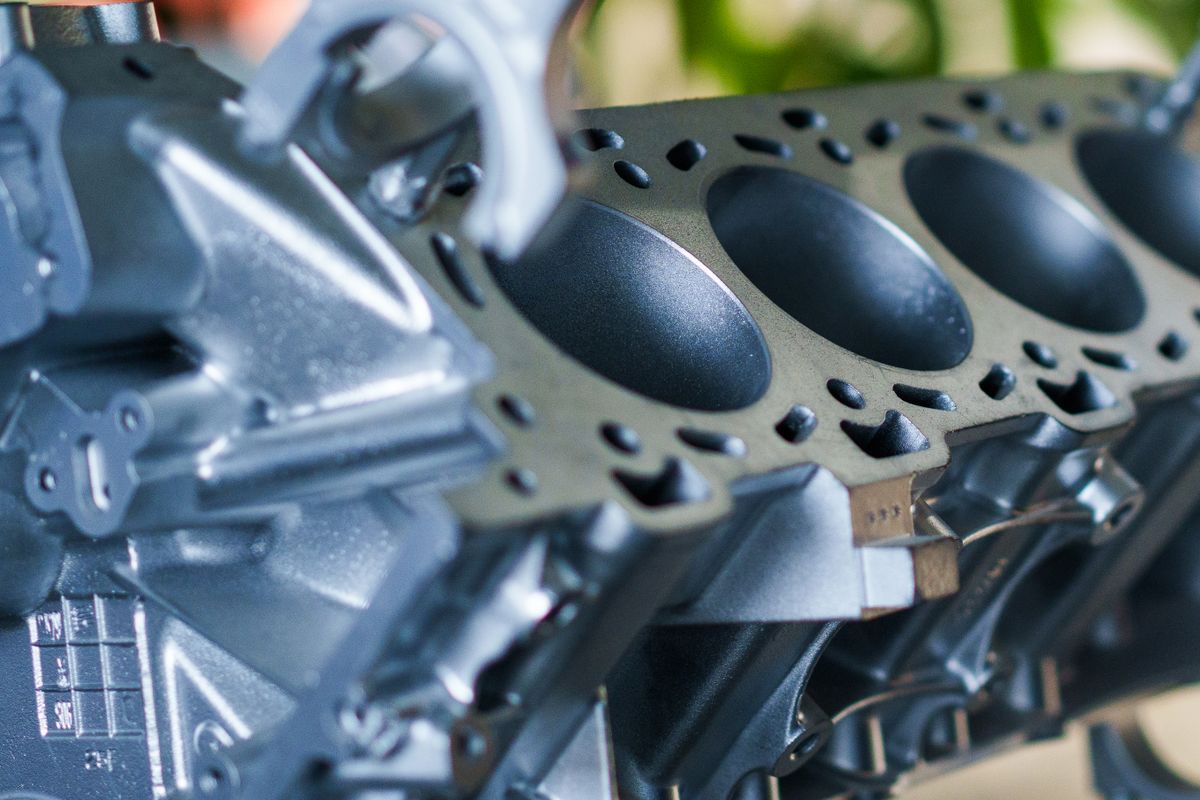
Engine block with cylinder bores in a workshop

Overview

The block is the foundation of every rebuild

The cylinder block carries the bores, the main bearing saddles and the deck that seals the head. If any of those reference surfaces are worn, tapered or distorted, no amount of new parts produces a durable engine.

Our block reconditioning route starts with a full strip and clean, then moves to inspection and precision measurement before any metal is removed. Machining is carried out to bring every critical surface back into specification and alignment for assembly.

Reconditioned to measurement

Reconditioned to measurement. Not guesswork.

Decisions on cylinder block reconditioning are made from recorded measurements against specification — never from how a part “looks”.

Inspect · Measure · Machine

Symptoms

When is this work needed?

These are the problems and symptoms that typically point to the component needing reconditioning work.

  • Excessive oil consumption with a compression-related cause
  • Blow-by or high crankcase pressure
  • Loss of compression across one or more cylinders
  • Coolant entering the oil or oil entering the coolant
  • Measured bore taper, ovality or visible scoring
  • Failed head-gasket sealing despite a true head

Sub-services

The cylinder block reconditioning jobs covered

Each item is listed so you can see the full scope of this service. Machining jobs run through PRT's inspect, measure, machine and verify route; specialist processes that are arranged externally are called out in the notes.

Cylinder block

  • Cylinder block inspection
  • Cylinder boring
  • Cylinder honing
  • Cylinder re-sleeving / liner replacement
  • Dry liner fitting
  • Wet liner fitting
  • Cylinder block resurfacing
  • Line boring
  • Main bearing housing / tunnel reconditioning
  • Camshaft bush boring / line boring
  • Block crack checking
  • Block crack repair
  • Block pressure testing

Inspection

Inspected and measured before machining

5 checks and measurements inform the decision to machine — nothing is cut until the component has been assessed.

  • Cylinder bore size, taper and out-of-round at multiple depths
  • Deck flatness and surface condition
  • Main bearing bore sizes and alignment
  • Crack detection by the method appropriate to the casting
  • Water jacket and oil gallery condition after cleaning

Measurement & quality

Measured, then machined to size

Bore and deck decisions are driven by dial-bore and straight-edge measurement against the component's specification — not by guesswork.

Verified after machining

  • Bore geometry recorded per cylinder, per depth
  • Deck flatness verified before and after surfacing
  • Main bore alignment confirmed where line boring is required

PRT process

How we carry out the work

  1. 01

    Receive & record

    Strip-inspection confirms the block identity, original size and what the rebuild needs to deliver.

  2. 02

    Disassemble & strip

    Core plugs, gallery plugs and remaining hardware are removed before hot cleaning.

  3. 03

    Clean & inspect

    The block is cleaned and checked for cracks, porosity and damage.

  4. 04

    Measure

    Bores, decks and main saddles are measured to decide the machining required.

  5. 05

    Machine

    Boring, honing, surfacing and line boring are carried out in sequence to keep features square and aligned.

  6. 06

    Final prep

    A final clean and assembly preparation leaves the block ready for building.

Machinery & stations

Performed at the right station, with the right tooling

Each operation is carried out at the appropriate station with the correct tooling. The stations involved in this service are:

  • Cylinder boring & honing station
  • Surface/deck machining station
  • Line boring set-up
  • Precision measuring & gauging area

Gallery

From the PRT shop floor

Authentic PRT photography of real jobs will appear here as it is captured and approved.

Shop floor

Cylinder Block Reconditioning work in progress at the PRT facility.

Machining close-up

Real photography of the operation will appear here when PRT approves imagery.

Finished result

Before-and-after records of PRT jobs are published as real projects.

FAQ

Common questions

Straight answers to the questions we expect about this service.

When does a cylinder block need reconditioning rather than replacement?

When the casting is sound but the bores, decks or main bearing housings are worn or distorted, reconditioning restores the block to specification at a fraction of replacement cost.

Do you machine to a standard size or an oversize?

The block is measured first and machined to the size the rebuild requires — standard, or the appropriate oversize matched to new pistons and rings.

Is line boring included with block reconditioning?

Line boring of the main bearing housings is performed when measurement shows alignment or size is out. It is assessed during inspection and confirmed before machining.

Get a Quote

Discuss a cylinder block reconditioning job

Tell us the engine or component, its condition and what the rebuild needs to achieve. We will confirm the scope from an actual assessment.